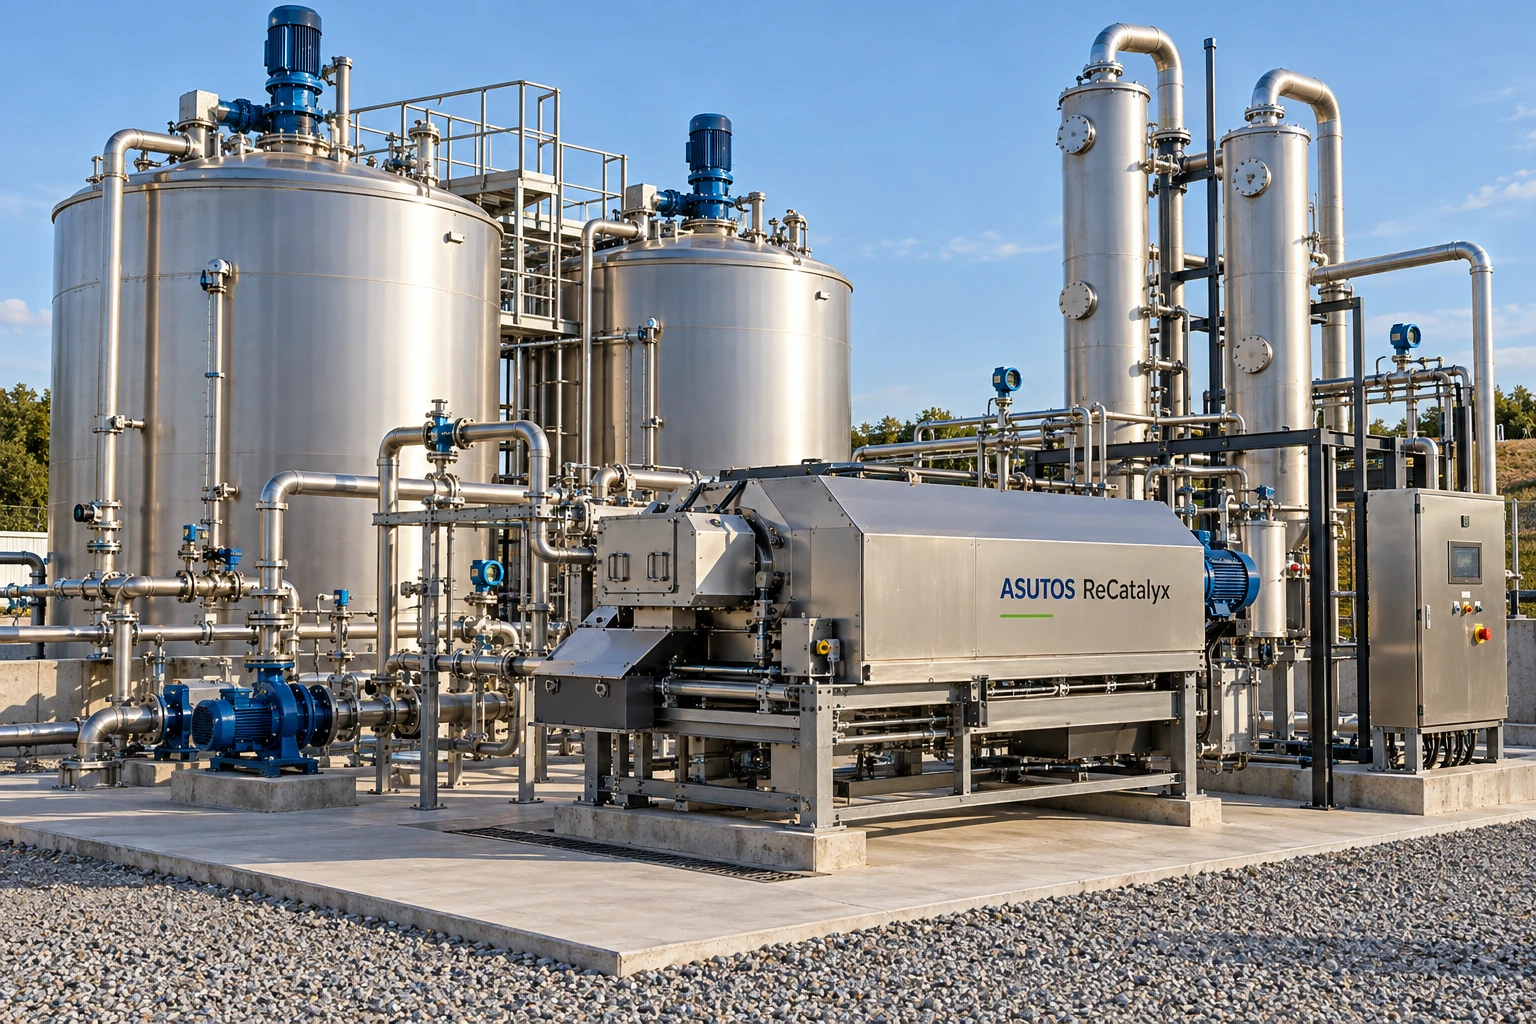
ReCatalyx
ReCatalyx GasBoost
Deliver conditioned gas at the required pressure.
- Brand
- ReCatalyx
- Discipline
- Carbon, Resource Recovery & Waste-to-Energy
- Markets
- Environment · Industry · Resources & Waste · Water & Utilities
- Development status
- Product concept
Overview
Deliver conditioned gas at the required pressure.
Product capabilities
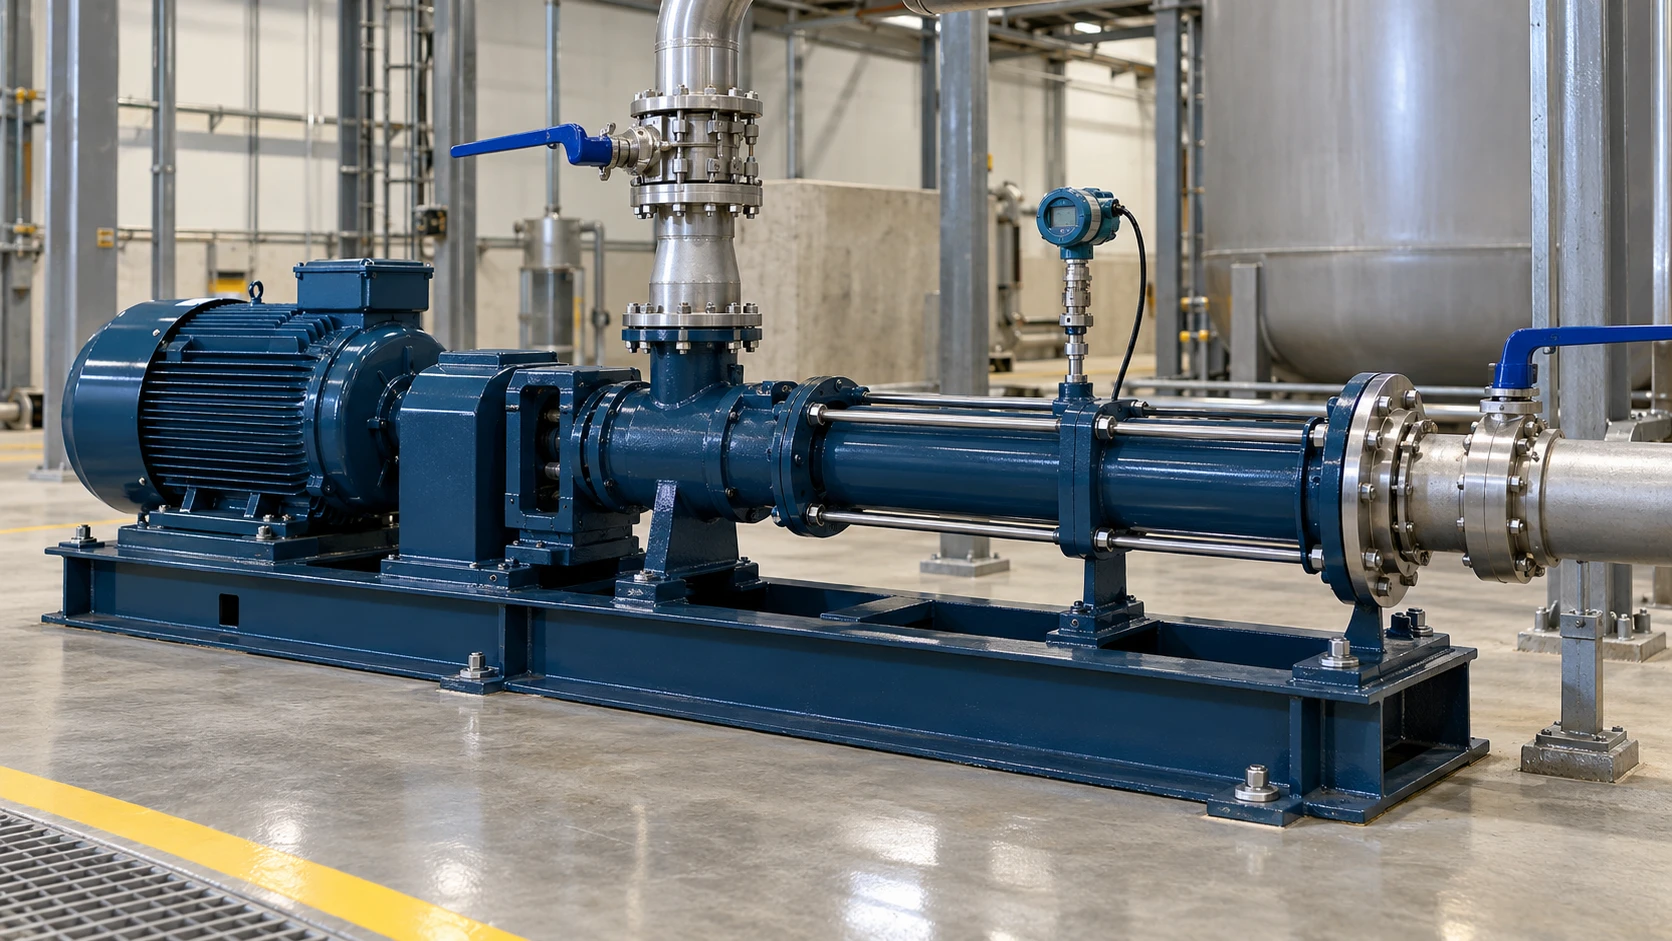
- Qualified blower or compressor
- inlet filter
- intercooling where required
- separator
- anti-surge or recycle and shutdown valves
Core components
- Qualified blower or compressor
- inlet filter
- intercooling where required
- separator
- anti-surge or recycle and shutdown valves
Design basis
Composition, suction pressure, turndown, outlet pressure and hazardous area; gas-compatible seals and OEM rotating assembly.
IoT measurements
Pressure, temperature, flow, vibration, load and seal condition.
IoT architecture
Project-specific instruments connect to local PLC/HMI and a secure gateway with buffered history. Local control remains independent of cloud connectivity.
Typical applications
RNGPure, LandfillGas, H2Recover
Pilot validation
Final sizing, protection and acceptance criteria require the project datasheet, OEM qualification and agreed FAT/SAT tests.
Problem and deployment scope
Deliver conditioned gas at the required pressure.
How it works
- Qualified blower or compressor
- inlet filter
- intercooling where required
- separator
- anti-surge or recycle and shutdown valves
Architecture
Confirm data sources, field interfaces and operating requirements during discovery. Integration compatibility is reviewed for each deployment.
Integrations
Interface availability and supported protocols require product-specific confirmation.
Deployment
Scope, installation, security, acceptance criteria and training are agreed with the project team.
Use cases
RNGPure, LandfillGas, H2Recover
Documentation
This page describes the published product concept. Validated drawings, datasheets, compatibility and deployment documentation are supplied following technical review.