ReCatalyx
ReCatalyx Digestate
Resource recovery and useful heat
- Brand
- ReCatalyx
- Discipline
- Carbon, Resource Recovery & Waste-to-Energy
- Markets
- Environment · Industry · Resources & Waste · Water & Utilities
- Development status
- Product concept
Overview
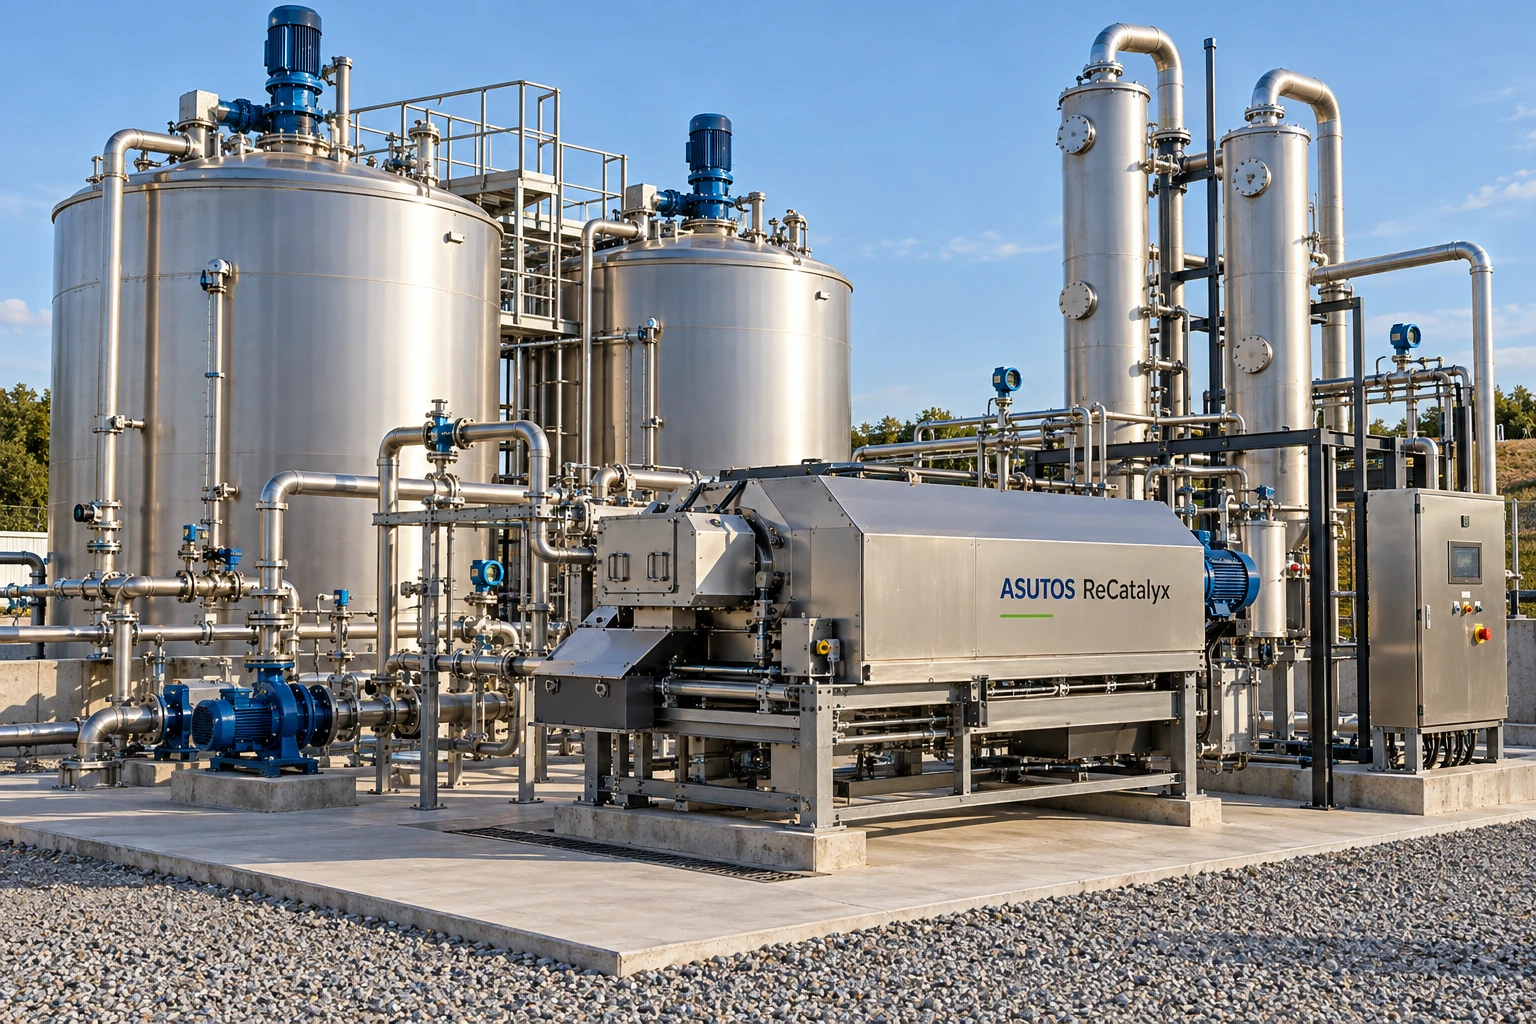
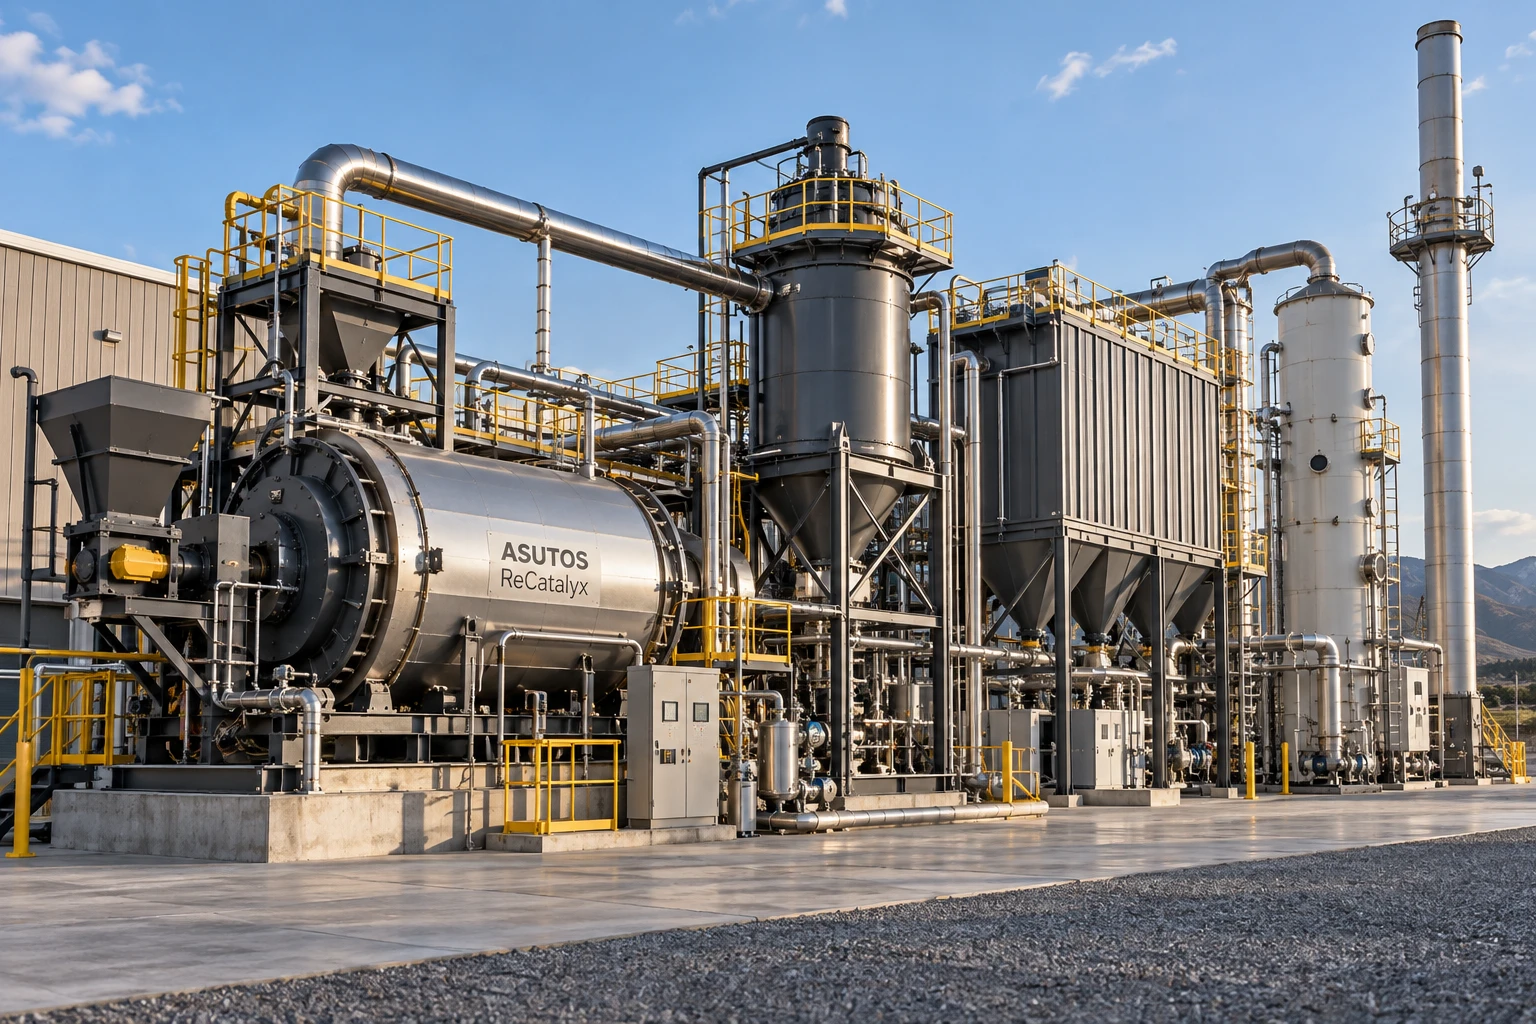
A digestate conditioning and nutrient recovery package that manages the liquid and solid outputs from BioDigest. It can combine solids separation, controlled composting or drying, nutrient recovery and liquid polishing according to the outlet. Digestate is not automatically an approved fertilizer, especially when biosolids are included.
Product capabilities
- Buffer tank
- polymer dosing if required
- screw press, belt press or decanter
- solids conveyor
- optional composting or drying
- nutrient recovery reactor
Feedstock and input
Characterized digestate with measured nutrients, pathogens, metals and relevant contaminants.
Core components
- Buffer tank
- polymer dosing if required
- screw press, belt press or decanter
- solids conveyor
- optional composting or drying
- nutrient recovery reactor
- liquid treatment
- odor management
- sample points
- storage and controls
Process
Separate digestate; condition solids; recover selected nutrients; treat or reuse liquid under approved conditions.
Design basis
Confirm nutrient balance, outlet quality, seasonal land access, wastewater loading, chemical use and residue transport.
IoT measurements
Flow, dry solids, separation performance, dosing and storage; link nutrient and contaminant laboratory results.
IoT architecture
Local PLC/HMI, buffered historian and secure gateway; remote alarms and reports. Cloud loss does not stop local control. See common architecture and acceptance tests.
Future capability
Flag unusual nutrient and separation results and reconcile weighed product movements.
Typical applications
U.S. farms and organic waste processors; global digestion plants with approved nutrient or material outlets.
Pilot validation
Demonstrate outlet testing, odor management, pathogen controls as applicable and lawful reuse or disposal records.
Problem and deployment scope
Resource recovery and useful heat
How it works
- Buffer tank
- polymer dosing if required
- screw press, belt press or decanter
- solids conveyor
- optional composting or drying
- nutrient recovery reactor
Architecture
Confirm data sources, field interfaces and operating requirements during discovery. Integration compatibility is reviewed for each deployment.
Integrations
Interface availability and supported protocols require product-specific confirmation.
Deployment
Scope, installation, security, acceptance criteria and training are agreed with the project team.
Use cases
U.S. farms and organic waste processors; global digestion plants with approved nutrient or material outlets.
Documentation
This page describes the published product concept. Validated drawings, datasheets, compatibility and deployment documentation are supplied following technical review.